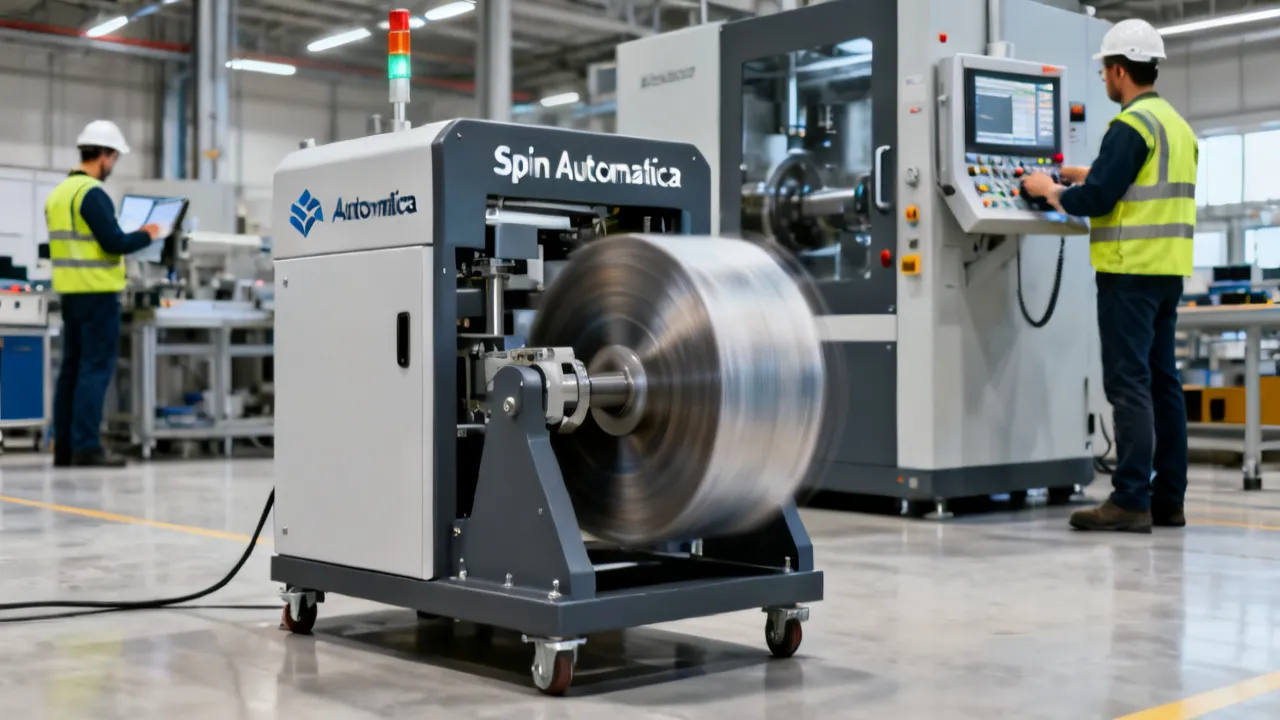
Spin Automatica technology is examined here with a practical, decision-oriented lens for operators and buyers. Objectively, the term is commonly used in industrial settings to describe automated systems that manage spinning or rotational workflows with repeatable controls. The guide outlines selection, integration, and quality considerations, with a later section comparing typical options, key sources, and requirements.
Spin Automatica systems are typically evaluated for how reliably they execute rotational processes, how consistently they deliver results across batches, and how maintainably they fit into existing production lines. If you’re researching or specifying a Spin Automatica solution, the very important early questions are: what rotational tasks are required, what tolerances define “acceptable,” and which operational constraints (cycle time, material handling, safety interlocks, traceability) determine whether the installation performs as intended.
From an industry-expert standpoint, the top outcomes usually come from treating Spin Automatica as a controlled process—not just a machine purchase. That means mapping the process from input to output, then validating whether the automation strategy can reproduce performance across real operating conditions (shift changes, material variability, wear over time, and maintenance schedules). It also means defining what “repeatable” really means to your product, to your downstream quality metrics, and to your operators. A system can be mechanically capable yet still fail as an operational system if the data flow, safety logic, and maintenance cycle are not designed with production reality in mind.
To make this concrete, consider how “rotation” affects results: rotational speed, acceleration/deceleration, duration, and load stability can all influence mixing uniformity, surface exposure, coating thickness distribution, drying behavior, abrasion patterns, and defect creation. Many of those outcomes are not purely physical—they are statistical. Therefore, your specification should aim to bound variability, not only to hit nominal targets.
Finally, early planning should include the human factors of automation. Operators need clear alarms, intuitive HMI screens, and predictable recovery procedures after faults. Maintenance staff need access, documented service tasks, and a clear understanding of what “calibration” means for your particular equipment. Without this, a system may look successful during acceptance testing and then drift into unreliable performance during routine production.
“Spin Automatica” is often used as a label or shorthand within industrial and manufacturing contexts for automated equipment that performs spinning, tumbling, or rotational handling under programmable control. While specific product designs vary widely by supplier and application, the underlying engineering themes are consistent: rotational motion is controlled precisely; process states are sequenced via automation logic; and results are managed through sensors, measurement routines, or downstream quality checks.
In general industrial practice, rotational workflows are used when materials benefit from even distribution, surface action, consistent mixing behavior, or uniform exposure to subsequent steps (for example, coating, drying, curing, inspection, or finishing—depending on the industry). Automation is then introduced to reduce variability, improve throughput, and maintain repeatability under defined parameters.
However, rotational automation often hides complexity. A rotation stage is not just a motor spinning a container. It can include fixturing geometry, rotating fixtures, bearings and supports, dynamic balance requirements, material-contact surfaces, drive coupling and backlash management, load sensing (direct or indirect), and an operational sequence that accounts for start-up conditions (e.g., empty-to-loaded transition, temperature soak time, ramp/settle requirements). The “automation” part then ties all of this to recipes, interlocks, safety logic, data capture, and production scheduling.
Because rotational processes are sensitive to mass distribution, many systems incorporate strategies such as controlled loading procedures, orientation control, dwell times, and sometimes closed-loop control using speed feedback or load-related signals. Even with these strategies, outcomes depend on real-world inputs—like differences in material particle size distribution, moisture content, part-to-part geometry variation, and the presence of residue buildup over time.
Therefore, when you read “Spin Automatica” on a datasheet or vendor brochure, it is best treated as a category descriptor rather than a guarantee of specific performance. Your job is to translate what the category implies into your process reality, then demand evidence that the system can meet your targets while remaining safe and maintainable.
When buyers compare Spin Automatica solutions, they often focus on visible features (motor size, cabinet design, throughput claims). However, the decisive factors are usually less obvious and show up in the total system behavior:
These considerations are where operational risk is managed. If a Spin Automatica system is assessed only on speed, it may underperform in consistency—especially when inputs vary from batch to batch or when the line runs beyond initial commissioning conditions.
Marketing labels often compress multiple technical details into a single phrase like “high repeatability” or “precision control.” But repeatability is not a property of a motor alone; it is the combined result of mechanical design, control strategy, tuning, sensor accuracy, and operating discipline (loading procedure, maintenance intervals, and correct recipe selection). If any component is weak—such as loose tooling, poor sensor mounting, or insufficient data validation—repeatability will degrade in the production environment.
Another common trap is comparing throughput on a best-case basis. Rotational automation may have a cycle time that appears fast when tested with nominal conditions, but real cycle time can be dominated by loading time, recipe change overhead, ramp-up/ramp-down profiles, safety interlock verification, cleanout cycles, or recovery steps after fault events. Buyers should analyze the distribution of cycle time and downtimes, not only the average.
In addition, the “integration readiness” category deserves more attention than is often given. A system can be technically excellent but still cause operational problems if it cannot reliably coordinate start/stop states, handshake with upstream/downstream equipment, or provide consistent fault codes and logging. In regulated environments or in processes with customer quality requirements, data capture and traceability can be as critical as physical performance.
Very organizations adopt rotational automation to achieve one or more of the following outcomes:
To evaluate whether a specific Spin Automatica configuration can meet these objectives, you’ll want evidence from commissioning results, acceptance tests, and documentation about control logic behavior under fault conditions.
“Repeatability” in particular should be interpreted in relation to your quality mechanism. For example, if your rotational stage is meant to create uniform surface finish, you should not only measure rotation speed stability; you should measure a surface property distribution (even if via periodic sampling or inline imaging). Similarly, if rotation is meant to mix components, you should validate uniformity metrics and their correlation to rotation parameters.
Quality assurance is also affected by the operational concept of “batch.” Some processes treat one run as a batch; others treat multiple cycles within a batch, each with potential minor variations. Your batch record should capture the correct recipe ID, parameter values, key sensor readings, and any alarms encountered (even if the cycle completes). If a system discards error details or only logs minimal events, your ability to investigate quality deviations is reduced.
Operator efficiency is another goal that can be overlooked. If operators must manually intervene frequently to correct alignment, restart after recoverable alarms, or verify parameters on multiple screens, the automation can become a source of delays and errors. A good deployment includes human-centered design: clear prompts, sensible defaults, guided troubleshooting, and a straightforward method to confirm correct recipe selection.
Finally, safety and compliance should be addressed early. Rotational equipment includes mechanical hazards (pinch points, rotating parts, ejection potential), energy sources (kinetic energy in rotating mass), and electrical hazards. Even if a system is certified, you still need to validate that it operates safely within your facility context: how guards are installed, how emergency stops behave across the integrated line, and how interlocks interact with upstream equipment.
In practice, teams validate performance using structured acceptance criteria. Rather than relying on generalized claims, an expert approach is to:
This evaluation method supports informed decisions and aligns with general good practice in industrial automation commissioning and safety management.
To avoid overclaiming, it helps to ask vendors for the “evidence behind the claim.” If a vendor says repeatability is within tight tolerances, ask:
Another important consideration is statistical significance. A vendor may demonstrate excellent performance for a small sample size. Your acceptance plan should include enough cycles to detect meaningful variability and to confirm that the performance distribution stays within your tolerance bands.
Fault recovery behavior deserves special attention. Many systems complete a normal cycle reliably, but when something goes wrong—like a sensor fault, unexpected load condition, misaligned part, or a communication timeout—the system might halt in a way that is not practical for production. Worse, it might restart without restoring a safe baseline state. Your acceptance criteria should include how the system reacts to each category of fault, and what is required to resume production (manual reset, automated retry, recipe re-approval, or full line intervention).
Documentation quality is also a performance factor. A system that is difficult to troubleshoot, with incomplete electrical diagrams or missing safety function descriptions, can lead to long downtime. Buyers should treat documentation as a deliverable, not an afterthought.
You asked for price information and supplier details to be integrated. However, no specific price figures, currency, or named suppliers were provided in your prompt. In that situation, the very objective approach is to treat “price” as a variable dependent on configuration and scope, and to show how buyers can structure quotes so the cost reflects what actually matters.
When requesting a quotation for a Spin Automatica system, cost typically depends on:
For supplier selection, look for evidence of process experience in a comparable industry context, not just a generic automation capability. Ask the supplier to describe prior deployments similar to your workload—especially around rotational stability, material handling robustness, and service turnaround time.
To make cost comparisons fair and defensible, you should request a quote structure that separates:
This approach prevents “hidden scope” where a low hardware price turns into a much higher total project cost due to integration or safety validation gaps. It also clarifies ownership: who is responsible for integration testing, who provides safety validation evidence, and who supports troubleshooting if production deviates from acceptance conditions.
In addition, cost of ownership should include downtime and changeover overhead. A system might have a slightly higher initial price but reduce unplanned downtime or shorten changeovers via better fixture design and recipe management. In many production environments, those operational benefits dominate the total cost over time.
If your facility runs multiple shifts, consider support logistics. Vendors that can provide quick remote diagnostics, on-site service availability, and replacement parts within predictable lead times reduce downtime risk. For rotational systems, wear parts can require planned replacements. Having a reliable spare parts strategy (and a vendor that can supply consumables at the right time) often matters as much as the base equipment cost.
Spin Automatica success is often determined by what happens before and after the rotational stage. A professional integration plan should cover:
From the perspective of industrial operations, safety is not a checkbox. It is a system behavior that must be validated through appropriate testing and maintained with defined routines.
Integration details often determine whether automation is stable during real production. Key points to address include:
Traceability can be particularly challenging. Many systems log recipe IDs but not all relevant parameter details. Others log raw sensor values without a clear mapping to quality-related outcomes. You should define a minimal data set required for investigations and for customer/regulatory compliance. That data set should include:
Safety integration is equally important. Even if safety functions are implemented according to standards, their integration must be validated in your system context. For example, emergency stop devices must behave predictably across the entire line, and interlocks must prevent unsafe motion under any realistic fault condition. You should also confirm that the system’s “safe state” is well-defined: what motion stops, what power remains, and what conditions allow restart.
Below is a general, step-by-step guide you can use to structure commissioning and internal acceptance. Because exact functions vary by design, adapt details to the supplier documentation and your risk assessment.
Document what “spin” means in your workflow: target speeds, rotation profiles (constant, ramp, pulsed), duration, load mass, part orientation, and any constraints about surface contact or contamination control. This is also where you define what should happen during abnormal conditions.
In addition to the basic parameters, consider operational edge cases:
These questions shape control logic requirements and influence acceptance testing design.
Set acceptance thresholds for the rotational stage outcomes. Where possible, include multiple batches and include worst-case inputs (upper/lower tolerances of material properties).
An acceptance plan should include:
If your process is sensitive, you may need to include not only “normal” operation tests but also stress tests: long runs to reveal drift, repeated recipe changes to reveal state handling errors, and controlled fault injection to reveal whether the system transitions safely.
Check alignment, mounting stability, fixture condition, and whether the rotational assembly exhibits acceptable vibration and noise characteristics under load.
Mechanical checks should also consider wear and serviceability. For example:
Because rotational systems can be sensitive to imbalance, you should also define what happens when the system detects abnormal vibration or torque/load levels. Does the system reduce speed, pause for inspection, or shut down? Your acceptance plan should confirm the expected action.
Confirm that the control system correctly executes sequences, recipe parameters are interpreted consistently, and any alarms or sensor states map to the correct operational response.
Recipe validation should include:
Control logic should also handle transitions cleanly. For example, if the line stops mid-cycle, the system must define whether it safely returns to idle, how it preserves the batch record, and what is required before resuming. Poor state management can lead to incorrect data association (e.g., logging parameters for the wrong part/lot).
Run the safety validation tests described in your functional safety plan. Confirm emergency stop response times, interlock enforcement, and safe state behavior during abnormal conditions.
Safety checks should not only verify that the emergency stop works, but also that safety interlocks enforce motion prevention during guarded access situations. You should test scenarios such as:
Also confirm that safety-related documentation matches what is installed. Differences between design and as-built wiring or parameterization can undermine safety performance. During commissioning, compare the safety function test results to the safety requirement specification and validate that the achieved performance meets the required safety integrity targets.
Test the full line interaction: start/stop handshakes, buffering behavior, and how the system handles upstream/downstream stoppages.
Integrated trials should include scenarios that stress the system’s operational logic:
These tests help ensure that the system is not only mechanically correct, but operationally robust as part of the production ecosystem.
Ensure operators can handle normal adjustments, alarms, and controlled transitions. Set maintenance intervals for wear parts and establish calibration and verification tasks.
Training should cover:
Maintenance routines should include planned inspections for mechanical wear, sensor validation steps, and cleanliness checks. For rotational processes, cleanliness can be a performance factor; residue buildup can alter balance, friction, and effective contact behavior.
Implement configuration management for recipes and control settings so that future modifications are reviewed and validated against acceptance criteria.
Change control prevents subtle drift. For example, if a parameter is updated to improve yield but not revalidated, you can introduce quality variability or safety risk. Your change control process should define:
In regulated environments, change control also supports audit trails and compliance.
Regardless of supplier, reliable operation typically requires that the system’s assumptions match real production conditions. Consider the following conditions:
These requirements are the practical bridge between design intent and good performance.
It is useful to think of reliability as layered. Layer one is the mechanical layer: stiffness, balance, bearing health, and alignment. Layer two is the control layer: sensor accuracy, control tuning, and recipe correctness. Layer three is the operational layer: loading procedure, maintenance discipline, and operator adherence to mode switching and safety rules. If any layer is weak, the system will behave less predictably.
Input loading stability is often underestimated. Many rotational processes require a fairly consistent initial mass distribution; if upstream handling introduces variability (e.g., parts tumble in random orientations within a loading fixture), the rotational outcome may vary. If redesign is not possible, you may mitigate variability through improved fixturing, sensor-based detection of load conditions, or control logic that compensates for detected differences.
Cleanliness management should be treated as a preventive maintenance strategy, not just housekeeping. Residue can change effective friction and alter torque requirements, which may degrade control performance. It can also increase imbalance risk and affect vibration. Therefore, define cleaning intervals and cleaning procedures that are consistent, documented, and validated to restore the equipment to a known performance baseline.
Environmental constraints matter for electronics and sensors. For example, vibration levels can be affected by facility floor conditions, nearby equipment, and HVAC effects that influence cabinet temperature. If your rotational automation is installed on a shared area with other rotating machinery, you should assess potential resonance or vibration coupling issues during commissioning and consider mitigation strategies.
Sensor performance is critical if you use feedback control. If speed feedback sensors drift or if vibration sensors are miscalibrated, the control system may “correct” in the wrong direction. Even if closed-loop control is used, sensor accuracy limitations can create variability. Your maintenance plan should include periodic verification of sensors used for process control or monitoring.
Wear and drift management ties it all together. Rotational systems often experience wear in bearings, drive couplings, seals, and mechanical fixtures. Over time, wear can change vibration patterns and affect stability. A reliability-minded deployment includes trend monitoring (e.g., track vibration and torque signature over months) and uses that data to schedule maintenance before performance drifts out of acceptance thresholds.
| System Option | Top Fit Scenarios | What to Validate in Trials | Operational Trade-offs |
|---|---|---|---|
| Closed-loop rotational control (with feedback) | Processes needing tight speed stability and consistent outcomes under load changes | Control bandwidth, stability under different loads, drift behavior over time | More instrumentation and calibration effort; potentially higher upfront complexity |
| Recipe-driven automation (parameter sets) | Multiple SKUs or frequent product changeovers | Recipe change accuracy, logging completeness, deterministic sequencing | Requires strong recipe governance and training to prevent incorrect parameter selection |
| Inline integration with quality data capture | Where the rotational stage affects downstream inspection or rework rates | Data consistency, batch traceability, correlation between settings and outcomes | More integration work; needs data model alignment with MES/SCADA or historian |
| Robust mechanical design for harsh material environments | When residues, abrasion, or chemical exposure are meaningful risks | Wear profile, cleaning access, surface compatibility, noise/vibration trends | May increase maintenance frequency or require specialized consumables |
| Modular fixtures and tooling strategy | Frequent format changes or multiple part geometries | Repeatability across fixtures, setup time, and alignment repeatability | Tooling inventory management becomes a key part of operations |
Choosing among these options should be driven by process sensitivity and operational complexity. For example, if your product outcome is highly sensitive to rotational speed and load variability, closed-loop control and robust mechanical balance may be worth the additional complexity. If your main challenge is changeover overhead and operator error, recipe governance and modular fixturing might provide better ROI.
Another selection criterion is the maturity of your data infrastructure. If you already have a strong MES/SCADA/historian platform, you can leverage inline data capture for stronger traceability and faster root cause analysis. If your data systems are still evolving, you may need to prioritize a minimal data set and a consistent logging strategy to avoid building a complex but unusable data pipeline.
Also consider operational ownership. A system option that is powerful but difficult to maintain can create hidden costs. If maintenance staff do not have the training or access needed to service the more complex components, you may experience downtime or performance drift. Therefore, validate not only what the system does, but what it takes to keep it doing it reliably.
Note: These standards provide general safety and design frameworks. Your specific Spin Automatica installation should be assessed through your own risk assessment and supplier documentation.
Even when standards are used as references, the as-built system still requires specific verification. A supplier may provide documents that reference safety standards, but your project team must ensure that the system is integrated correctly into your line. This includes verifying wiring, safety PLC configuration, safety-rated component selection, and safety function logic. Additionally, if your facility has unique hazards (e.g., chemical exposure, dust hazards, additional energy sources), you may need to augment the risk assessment beyond the baseline framework.
For automation and data reliability, consider also relevant best practices in industrial automation engineering such as disciplined version control for control software, consistent naming and documentation standards for I/O and signals, and calibration traceability for measurement instruments. While not “safety standards,” these practices significantly affect the ability to reproduce outcomes and investigate deviations.
In many industrial contexts, it refers to automated equipment that performs spinning or rotational operations under programmable control. The exact mechanism, sensors, and control logic depend on the supplier and the process requirements of your line.
Because “Spin Automatica” can be used as an umbrella term, it’s important to clarify the specifics: Is it a bowl/tumbler system, a spindle-based system, a rotational fixture with clamping, or a multi-axis rotation stage? Does it include speed feedback, vibration monitoring, or torque/load detection? Your technical specification should answer these questions explicitly rather than relying on the shorthand label.
Look beyond purchase price. Include commissioning effort, integration work, maintenance access and consumables, calibration tasks, downtime risk, and training. A quote should clearly distinguish hardware supply from integration, safety validation, and service support.
To estimate total cost of ownership (TCO), you can create a cost model that includes:
The goal is to compare suppliers and configurations on a like-for-like basis. A higher upfront system cost might reduce downtime and increase yield, lowering TCO.
Usually yes, but integration readiness must be verified: compatible I/O, communication protocols, safety interface strategy, and the ability to coordinate start/stop and fault states with upstream and downstream equipment.
Integration also includes how your line schedules tasks. If your upstream equipment triggers the rotational stage based on part presence detection, you must ensure timing alignment. If downstream equipment rejects parts based on quality measurement, you must understand how that rejection influences rotational stage behavior (e.g., whether the system counts the cycle as complete, whether it logs rejection, and how it handles subsequent batches).
Request metrics relevant to your outcomes—such as cycle time distribution, stability under load variation, repeatability across batches, fault recovery behavior, and evidence of traceability if quality is tied to the rotational parameters.
Depending on your process, consider asking for:
It is critical. Rotational systems include mechanical hazards and energy sources, so safety interlocks, emergency stop behavior, guarding, and validated safety functions should be addressed through recognized safety engineering practices.
Functional safety is not only about preventing immediate injury; it also supports process robustness. A well-designed safety system reduces nuisance trips and clarifies operational modes. A poorly designed safety system can cause frequent stops and create workarounds that reduce safety. Therefore, functional safety should be evaluated as part of the operational performance, not only as compliance paperwork.
That depends on design and how feedback control is implemented. A professional supplier will provide a maintenance and verification schedule, including what needs calibration (if anything), how often, and how to confirm performance remains within specification.
Even if the system does not require frequent “calibration” of the rotational mechanics, you may need periodic verification of sensors and monitoring equipment (e.g., speed sensors, vibration sensors, load measurement transducers, or temperature sensors). The calibration regime should reflect the criticality of each measurement to the quality outcome.
Expect electrical documentation, control system documentation, safety-related descriptions, maintenance manuals, acceptance test records (FAT/SAT where applicable), and training materials that reflect real operating procedures.
In many successful projects, documentation is a deliverable with a defined completeness standard. Consider insisting on:
This reduces the risk of “tribal knowledge” where only one person understands the system.
To improve the usefulness of supplier responses, ask follow-up questions that force detail. For example, if a supplier claims “closed-loop speed control,” ask what feedback sensor type is used, how it is calibrated, what the measurement resolution is, and how the control loop is tuned. If a supplier claims traceability, ask what exact fields are stored per batch and whether alarms and operator mode changes are logged.
Also, ask about operational friction. How do operators start production? How does the system ensure the correct recipe is used? What is the expected time to recover after a fault? If troubleshooting requires complex manual steps, the system may become burdensome even if it performs well mechanically.
Spin Automatica evaluations should be anchored in measurable process requirements, robust commissioning practices, and a safety-focused integration plan. With a structured approach—defining acceptance criteria, validating control behavior, and confirming maintainability—teams can make confident decisions and reduce operational risk. While price and supplier offerings will vary, the very reliable path is to compare systems based on documented performance evidence, clear integration scope, and practical operational requirements that match your production reality.
Ultimately, “safe, repeatable automation” is not achieved by selecting a machine with impressive specifications alone. It is achieved by building a reliable system: a rotational stage designed to handle your loads and materials, a control and data layer that executes recipes deterministically and logs the right information, and a safety architecture that prevents hazardous motion while enabling practical recovery from faults. When these elements are aligned to your production environment, Spin Automatica can deliver consistent results—not just during commissioning, but throughout ongoing production, changeovers, and maintenance cycles.
Striking the Perfect Balance: Navigating Premiums and Out-of-Pocket Expenses in Senior Insurance Plans
Explore the Tranquil Bliss of Idyllic Rural Retreats
How to Make Lasting Memories at Disneyland Attractions
Affordable Phones and Plans for Seniors
Affordable Full Mouth Dental Implants Near You

Unlock the Top Kept Secrets to Finding Your Ideal Dentist for Flawless Dental Implant Results!
Discovering Springdale Estates
The Guide to Car Trading
Affordable Cell Phones Without Plans
Unveiling Grunig & Hunt's PR Models
This article explores the seminal work of Grunig & Hunt in developing models of public relations. The Grunig & Hunt models, fundamental to understanding PR theory, provide insight into the strategic approaches and methodologies utilized in the field. Each model offers a distinctive perspective on communication and engagement strategies, relevant to both academic discussions and practical applications.
Understanding Attimo Family Office
Attimo Family Office represents a new trend in wealth management services, designed to serve high-net-worth families with personalized attention and expertise. These offices provide tailored financial, investment, and lifestyle management to ensure good wealth preservation and growth. Emphasizing trust, discretion, and bespoke solutions, they cater to the distinct needs of affluent families.
Navigating Attimo Family Office Services
Attimo Family Office is a specialized financial service provider dedicated to managing the complex financial needs of affluent families. By offering personalized advice tailored to each family's unique circumstances, they help in safeguarding wealth across generations. The concept of a family office has been increasingly embraced by high-net-worth individuals seeking tailored investment strategies, tax planning, and legacy management.
Understanding Grunig & Hunt's PR Models
This article delves into the renowned Grunig & Hunt models of public relations, highlighting their significant contribution to the field of strategic communication. Developed by James E. Grunig and Todd Hunt, these models have guided PR practitioners in understanding and executing effective public relations strategies. This guide aims to elaborate on each model, explore their application in real-world scenarios, and underscore their relevance in contemporary PR practices.
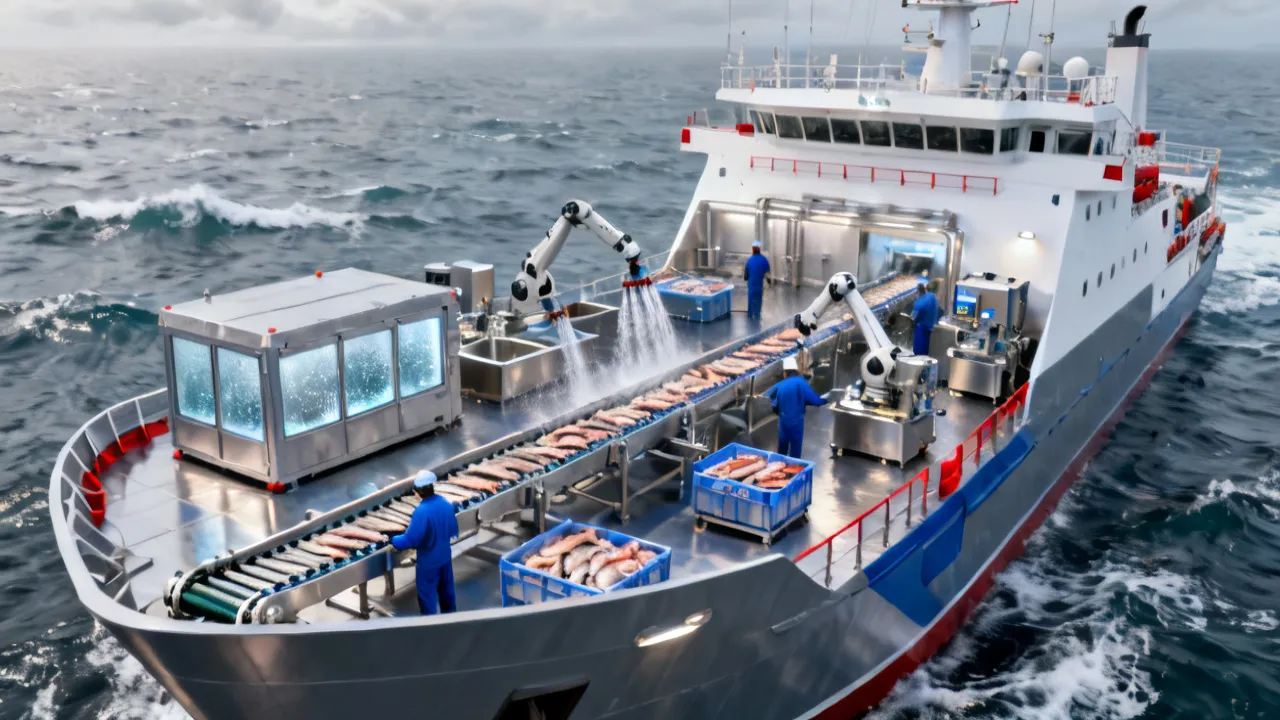
Unveiling the Optimar Rae
An in-depth exploration of the Optimar Rae, a frontrunner in seafood processing. Known for its advanced technology and efficiency, the Optimar Rae plays a pivotal role in modernizing seafood operations. This article delves into its significance, examining how it enhances productivity while maintaining environmental standards, marking a new era in maritime industry advancements.
Mastering Employee Retention Strategies
This article delves into the essential role of an Employee Retention Consultant. Employee retention is crucial for maintaining a competitive edge and fostering a positive work environment. Professional consultants help organizations in developing tailored retention strategies to reduce turnover, increase job satisfaction, and enhance overall productivity. Explore expert insights, strategies, and FAQs in employee retention.